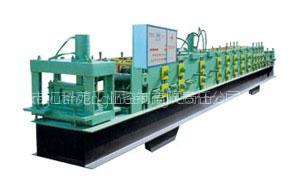
C-purlin machine
Specifications
- Brand
- Huikeyuan
- Origin
- China (Mainland)
C-purlin machine is a Industrial Power Supplies product. Key specs — Brand: Huikeyuan; Origin: China (Mainland).
Product Description
A basic knowledge of C-purlin machine Pressure-watt machine network: steel cut-off should be as far as possible cutting or sawing on the machine, especially for thin-walled steel roof truss, as required under the expected accuracy, the best use of electric sawing method, not only high efficiency, and smooth cross-section , good quality and length of the error can be controlled within ± 1mm or less.
If no equipment, but also can be used to improve gas cutting gas cutting quality, appropriate use of small diameter nozzle, and gently tapping with a hammer after cutting, so that incision formation, in order to clear the slag to ensure the welding quality. Light steel structures and general steel manufacturing process there is no significant difference.
Light steel material specifications is small, thin rods and thin, and the material transferred straight, blanking, bending and forming, processing, assembling, components turn over handling easy, does not require large specialized equipment, it is especially suitable for small and medium sized factories processing and manufacturing.
Round bar, the small angle of the light steel rods smaller, easy to shape, which is manufacturing advantage. However, in the course of processing are likely to cause rods bend and injury, etc., this bending and damage to the structure bearing capacity of large manufacturing should be noted.
Using cold-formed steel framing in general more than using a regular steel pickling, or pickling rust phosphating treatment process. When using 2 channel welding pipe welding Narikata large amount. As the rods connecting the top pick, mostly, it is expected under the higher accuracy requirements.
In the past people were worried that, cold-formed steel components thinner wall thickness, materials, straightening is not easy, but it proved its straightening process than ordinary steel is also easy to master.
Usually stays straight and stays straight machine with a hammer hammering on the platform in two ways: the former phenomenon is easy to adjust embossing, and can ensure quality.
For the truss-type purlins, roof, or spindle-shaped three-hinged arch roof, its continuous curved serpentine round steel belly bar with multiple births on hand at the completion of a smaller diameter, used cold-formed, larger diameter, the need to use oxygen acetylene local heating bending.
Cold and hot bending of the diameter of the boundaries of various manufacturing units with the specific circumstances of different bending radius of 2.5 times the diameter of round steel.
As the snake after the round bar in bending springback phenomenon, forming relatively large error after, so the positioning device with fetal ventral bar should be higher than the angles between the axis should be smaller, and later forming a model checking.
Welding is the main connection method of light steel structure, due to bar cross-section generally small, the thickness of thin, prone to welding distortion and burn, and therefore must pay attention to select the appropriate welding the welding process and welding parameters, such as electrode diameter, welding current size and welding procedures.
Welding parameters should be chosen depending on the thickness of welded parts and operations to determine skill levels. Commonly used electrode diameter φ3.2mm-4mm, the thickness of ≤ 2mm when the weld when the welding rod can be used φ2.5mm. At the same time pay attention to selecting a suitable welding current.
Current is too large, easy to burn, too small and easy to produce weld slag. Depending on the electrode diameter, Welding current 80A-200A in the context of changes, good welding technology, the current can be properly increased.
Welding shall be based on different nodes form, spatial location and welding pieces of thickness and correctly grasp the rod angle, welding method, welding speed and welding pieces of the temperature distribution in order to ensure quality of welding.
Should maximize the use boat-shaped flat welding and welding, For vertical welding, or horizontal welding, the welding should be skilled welders. In addition, should pay attention to the introduction of effective measures to prevent the welding deformation.
When several welder welding a component at the same time, the solder joints should be dispersed so that the heat uniformly throughout the component distribution; long seam welding method should be used reverse section.
A welded seam to be appropriate, such as the need in two welding should be cooled after the first weld seam second, not in a row to repeat on the short seam welding to prevent burn metal. The skill level of the welder should be certain requirements, Unskilled welders prone to bite of meat, pores, slag, crack, no welding defects such as full settlement tank.
Light steel bars are more dispersed solder joints, particularly should pay attention to check seamless welding and dislocation and so forth.
Related Products
 The new breakthrough in oversea buyers of HOSFAIR Guangzhou 2009
 APHSA will sponsor HOSFAIR Guangzhou
 jewejlry display
 watch display counter,watch display stand,display showcase,watch display cabinet
 watch display case,watch disply cabinet watch disply stand,counter and showcase
 Ningbo Medical Materials Co. Ltd.
 Provide ProTouch Nano Touch Foil(Interactive Foil)
 Provide Proshow Magic Window(Interactive Platform)